Get in touch with Zhenling Company
Industrial Electroplating Services for Precision Machined Parts
Electroplating services fail far more often on the machining table than they do in the tank. We machine the part, review the plating callout against the specification your customer named, and deliver the plated component as one line item. Electroplating Services enquiries should include substrate, applicable specification edition, thickness, masking, finish and buyer acceptance requirements. Schedule depends on the released inputs. Check route, limits, inspection evidence and exclusions before treating any date as firm.
-
ASTM B633
Service-condition classes SC1–SC4 read from the standard, not from a vendor page
-
5–25 µm
Zinc thickness band the four service conditions actually call for
-
8.0 µm
Practical ceiling on threaded articles before the pitch diameter is compromised
-
¼ allowance
ASME B1.1 rule for how much of the thread allowance a coating may consume
-
Written scope
Quotation identifies machining, finishing, drawing approval, records and handoff responsibility
-
Order-specific
Destination, packaging, export documents and delivery terms confirmed in writing
Most Plating Rejections Are Decided Before the Part Reaches the Tank
The failure everyone argues about after the fact
Plating can render a part unusable even when machining looked acceptable before finishing. That risk is why substrate condition, cleaning responsibility, critical surfaces and acceptance evidence should be agreed before the outside process begins.
Scrap arrives, the plater blames the substrate, the machine shop blames the bath, and the buyer is 10,000 km away with no way to referee. That argument is expensive because it starts after the money is spent.
Apply the ASTM B633 edition named by the customer. Substrate-defect and prime-contractor responsibility follow that edition, the purchase order and the written quotation; responsibility must not be inferred from a generic clause summary.
What clause 6.2 means for your purchase order
Read plainly, the standard puts substrate defects on whoever machined the part, unless the plater is the prime contractor. In a managed-subcontract model the machining shop is the prime contractor, so the responsibility doesn’t move at all, it stays with us, which is the whole reason the model works for a buyer.
Surface Condition Before Plating
Electroplating is a thin layer of metal grown out of an electrolyte onto a cathode, and that thin layer is a magnifier rather than a filler. An 8 µm zinc deposit doesn’t bridge a 30 µm tool witness mark; it decorates it. Every defect below is a machining-stage defect that only becomes visible after the finish goes on.
Failure mode → root cause → the control point that actually fixes it. Root causes compiled from a plating-defect field guide and cross-checked against ASTM B633 clauses 6.2 and 6.4.
What the buyer sees
Root cause
Control point
Blistering or peeling deposit
Oil, drawing compound or oxide film left in a blind pocket; adhesion never formed
Degrease and pickle routing written into the machining traveller, not left to the plater to guess
Dull or patchy coverage in a recess
Poor throwing power of an acid bath into deep geometry — current density collapses inside the feature
Bath chemistry chosen against the part geometry at drawing review; alkaline where full coverage inside recesses is required
Coating thinner than the callout at an internal corner
Electric current concentrates on edges and starves corners; the deposit follows the field, not the drawing
Significant surfaces marked on the drawing so the plater knows where the minimum is measured
Cracking days after delivery on a hardened part
Hydrogen absorbed during cleaning and plating, never baked out inside the window
Tensile strength and hardness stated on the drawing so the embrittlement relief requirement is triggered before, not after
Rack or contact marks on a sealing face
Every part is held somewhere; the holding point is bare
Contact-point zone nominated by the machine shop, in the one place that is not a functional surface
Complete finish callouts should define the substrate and process boundary before the part reaches the plater: An incomplete drawing that says only ‘zinc plate’ leaves chemistry, thickness, significant surfaces, post-treatment and acceptance criteria unresolved. This missing scope is the structural reason for the RFQ checklist on this page.
“
This page does not claim that Zhenling owns or does not own a plating line. The quotation must name the applicable specification, type, service condition, significant surfaces, outside-process responsibility and acceptance evidence before release.
Working from a drawing that says only “zinc plate”?
Send a Drawing for a Finish-Spec Review →
a specification read-back, with no quote attached.
Electroplating Finishes Available on Zhenling-Machined Parts
Six deposit families cover almost every callout that arrives with a machined steel or stainless component. Each one below states the composition band, the substrates it suits, and the named application it’s chosen for, in that order, because that’s the order an engineer decides in.
How to read this section
The quotation identifies whether each finishing step is performed internally or by a named outside processor, together with specification, responsibility, records and delivery scope. Published standard values do not establish a Zhenling process capability.
What a Deposit Adds to the Physical Properties of a Part
Plating is versatile because the deposit brings physical properties to a base metal that lacks them. Corrosion resistance is the reason most drawings call for it, and a corrosion resistant deposit on an inexpensive substrate is often better engineering than a corrosion-resistant alloy throughout.
Corrosion and wear: a sacrificial deposit slows corrosion while a hard barrier deposit slows abrasion, and one resistant coating rarely does both well
Tarnish and oxidation: tin and nickel keep a contact surface solderable by holding back the oxidation that would otherwise dull it
Lubricity: a deposit changes friction at a thread or a sliding face, which is why torque tables are written against a stated finish
Heat resistance: a diffusion barrier keeps two individual metals from alloying during heat treatment
Aesthetic appeal: an exterior finish is a durable appearance requirement, and it’s measured differently from a functional one
Substrate Notes: Stainless, Aluminium and Alloy Steel
Stainless 303, 304, 304L, 316, 316L and 321 need the passive oxide film activated first, usually with a nickel strike, or adhesion fails no matter how good the bath is
Aluminium alloys, written aluminum on US drawings, take a zincate immersion step before plating, and for many aluminium parts hard anodizing is the better route, which we’ll say at drawing review
High-strength alloy steel above 1000 MPa falls under ASTM B633 clause 6.4, which requires stress relief before plating for machined, ground, cold-formed or cold-straightened parts at that strength or above
Steel above 1700 MPa is excluded outright: clause 1.3 of the standard states these shall not be electroplated at all
On nickel-based alloys, C276 and 904L, which we machine for chemical service, the correct answer in most cases is no coating rather than a coating
Where these deposits apply, and where they do not
The commonly used metals for electroplating in industrial work are zinc, nickel, copper, tin and chromium, deposited from various metal salts. Precious and specialised work sits in different supply chains with different qualification routes: gold, platinum and palladium alloys, the plating used on jewelry, finishes applied to 3D printing output, surgical implant coatings where biocompatibility governs, and the deposits used on semiconductors and connectors. Titanium and aluminium parts, and anything selected for a high strength-to-weight ratio, usually route to anodic or conversion processes instead.
01
02
03
04
05
The Four Components That Decide Every Deposit
Every callout you write is an instruction to four things, and knowing which one your requirement acts on makes the drawing easier to specify. An electroplating process needs a power source, an anode, a cathode and an electrolyte solution. Deposition is metal ions crossing between them under an electrical current.
Component
What it does
What you control from the drawing
Power source
Drives the electrical current that reduces positive ions onto the part
Nothing directly, but current density is why a recess plates thinner than an edge
Anode
Supplies metal ions to the plating solution as it dissolves, or passes current inertly
The deposit metal: zinc, nickel, copper, tin
Cathode
The object being plated. Every surface must be electrically conductive for a deposit to bond to it
Base metal, surface condition, contact points
Electrolyte solution
Carries one or more metal salts so metal ions can adhere to the base metal
Alkaline or acid chemistry, driven by geometry and substrate
The Service-Condition Ladder
The Service-Condition Ladder — Gatto and other specification-anchored pages publish the two ASTM B633 tables separately. Chained into one decision path they answer the question a buyer actually has, which is not “what is SC3” but “what do I write on the drawing for a part that lives outdoors near salt”.
Service condition
Class
Min. thickness
Environment
Finish type
Min. salt spray
SC4 — very severe
Fe/Zn25
25 µm
Exposure to corrosive fumes, prolonged wetting, marine splash
Type VI, colored passivate
120 h
SC3 — severe
Fe/Zn12
12 µm
Outdoor, condensation, occasional wetting
Type II, colored chromate
96 h
SC2 — moderate
Fe/Zn8
8 µm
Mostly dry, occasional condensation
Type V, colorless passivate
72 h
SC1 — mild
Fe/Zn5
5 µm
Indoor, dry, warm
Type III, colorless chromate
12 h
Atmospheric corrosion rate of zinc, ASTM B633 Appendix X1: industrial 5.6 µm/yr · urban and marine 1.5 µm/yr · suburban 1.3 µm/yr · rural 0.8 µm/yr · indoors under 0.5 µm/yr
Chromate Conversion Coatings and Passivates
The chromate layer isn’t the corrosion protection; the zinc underneath is. What the conversion coating does is delay the onset of white rust on the zinc so the sacrificial layer isn’t spent before the part reaches service. This is the single most misread line on plating drawings we review.
Type
Finish
Min. salt spray, hours
Chosen when
I
As-plated, no supplementary treatment
no requirement
Part is painted or over-coated immediately
II
Colored chromate
96
General outdoor and condensing duty
III
Colorless chromate
12
Cosmetic or indoor, clear appearance required
IV
Phosphate conversion
no requirement
Paint adhesion base
V
Colorless passivate
72
Hexavalent-free clear finish
VI
Colored passivate
120
Highest thresholds in the standard, hexavalent-free
Barrel vs Rack: Which Fits Your Part
Selection is driven by geometry and by which surface must stay untouched, not by price alone.
Factor
Barrel plating
Rack plating
Part size and volume
Small parts, high count per load
Larger, heavier or awkward parts, individually held
Thickness uniformity
Tumbling averages the deposit; spread across a load is wider
Fixed position and controlled current path; tighter spread
Surface risk
Part-to-part impingement can mark a finished face
Contact points leave a mark where the rack holds
Typical machined-part fit
Plugs, small fasteners, bushes
Flanges, valve bodies, rollers, bent pipe, machined assemblies
Adjacent Metal Finishing Routes and When They Beat Plating
Electroplating is one branch of metal finishing rather than the whole of it, and part of a drawing review is saying when a different branch is the better answer. Buyers comparing electroplating processes against other plating techniques usually ask which one costs less. A more useful question is which one the geometry of the part allows.
Route
How it differs from electroplating
When it wins
Electroless plating
Autocatalytic rather than current-driven, so no anode and no power source
Deep bores and internal geometry where current density starves a corner
Powder coating
An organic film rather than a metallic deposit
Thick protective coatings and exterior colour where dimensional change is acceptable
E-coating
An organic film deposited electrically, so it follows current the way plating does
Complex fabrications needing uniform coverage before topcoat
Anodizing
Converts the substrate rather than adding a metal layer
Aluminium parts needing hardness and wear performance without a plated build-up
Passivation
Removes free iron and restores the passive film, adding nothing
Stainless parts where the correct answer is no coating at all
Not sure which of the six families your customer’s callout actually names?
Send a Drawing for a Finish-Spec Review →
Zinc vs Zinc-Nickel vs Electroless Nickel vs Hard Chrome
Choosing between deposits is a question about failure mode, not about which is “better”. Sacrificial coatings fail gradually and forgive damage; barrier coatings fail locally and punish it. Below we keep the numbers that come from a published standard and refuse to print the ones that don’t.
Comparison of the four deposits that dominate machined-part callouts. Cells marked “confirm against the named specification” are deliberately blank of numbers: we will not print a figure here that we have not read out of a standard, which is the same rule we apply to your drawing.
| Property | Zinc | Zinc-nickel | Electroless nickel | Hard chrome |
|---|---|---|---|---|
| Protection mechanism | Sacrificial | Sacrificial, alloyed | Barrier | Barrier |
| Governing specification | ASTM B633 / ISO 2081 | ASTM B841 | Autocatalytic nickel-phosphorus specification named by the customer | Engineering chromium specification named by the customer |
| Thickness the spec sets | 5 / 8 / 12 / 25 µm by service condition | Set by ASTM B841 class; confirm against the named specification | Confirm against the named specification | Confirm against the named specification |
| Minimum salt spray in the spec | 12–120 h by finish type | Suppliers cite roughly 5–6× zinc at equal thickness; not a contract term | Not expressed as a salt-spray threshold in the deposit spec | Not expressed as a salt-spray threshold in the deposit spec |
| Deposit hardness | Soft, ductile | 350–450 kg/mm² Vickers | Rises sharply after heat treatment; confirm against the named specification | The hardest of the four; confirm against the named specification |
| Coverage in deep recesses | Throwing power depends on bath; alkaline better than acid | Alkaline chemistry covers recesses well | Uniform without regard to current path — the reason it wins on complex geometry | Poor; current concentrates on edges |
| Thread and fit behaviour | Build-up consumes the allowance directly | Same build-up problem, plus higher torque for a given preload | Uniform build-up is easier to predict on a thread | Usually ground after plating rather than plated to size |
| Hydrogen embrittlement exposure | High on hardened steel; bake required | High; porous deposit is designed to vent hydrogen during bake | Lower — the process is autocatalytic rather than current-driven | High on hardened steel; bake required |
| Where it wins on a machined part | Volume steel parts in general industrial duty | Alloy-steel parts in marine, automotive and defense duty | Valve bodies and internal bores where uniformity matters more than hardness | Wear surfaces, hydraulic rods, shafts |
Decision route 1: the part sees weather and impact damage
Pick a sacrificial deposit and set the class from the atmosphere, not from a salt-spray target. A scratched sacrificial coating keeps working; a scratched barrier coating starts a pit at the scratch.
Decision route 2: the part has deep bores, blind holes or internal threads
Uniformity beats hardness. Compare against electroless nickel plating before committing to any electrolytic route, because current density is what starves an internal corner.
Decision route 3: the part is a fastener or has a fitted thread
The deposit thickness becomes a dimensional decision before it’s a corrosion decision. That’s the whole of the next section, and it’s where most of the money is lost.
Zinc-Nickel as the Cadmium Replacement
Zinc-nickel alloy plating has become the standard alternative to cadmium plating because the use of cadmium is restricted on toxicity grounds while the duty it covered didn’t disappear. A zinc-nickel coating built from zinc and nickel together gives superior corrosion resistance to zinc alone at equal thickness. That higher corrosion performance is what buys it a place in harsh environments.
What the alloy coating changes, and what it leaves alone
Alloy plating shifts the corrosion potential of the deposit itself, so the high corrosion performance is a property of the alloy rather than of extra thickness. Electroplated coatings of Zn-Ni still consume the same thread allowance as plain zinc, and they still need the same embrittlement relief on hardened steel. Any eco-friendly alternative framing around this finish applies to the trivalent passivate on top, not to the deposit underneath.
Salt-spray hours are often quoted without the specimen preparation, test method, duration owner, evaluation rule or acceptance value needed to interpret them.
How to Specify the Salt-Spray Requirement
Treat salt-spray results as evidence for the named test conditions and acceptance rule, not as a universal service-life prediction.
The standards agree by omission. ASTM B117 and ISO 9227 describe the apparatus and the method but set no test duration, leaving the hours to be agreed between customer and manufacturer.
The common assumption that does not survive the evidence
More hours doesn’t mean proportionally longer life. Hot-dip galvanizing lasts decades outdoors yet is destroyed quickly in a salt fog chamber, because the constant wetting never lets the stable carbonate corrosion products form. A finish can therefore lose the test and win the service life.
The Plating Tolerance Window: Specifying Machined Dimensions That Survive Plating
Every competitor page in this category publishes a thickness range. None of them tells you what to do with it on a drawing. The Plating Tolerance Window is the chain from nominal machined dimension through single-sided deposit to two-sided stack-up, and it’s the one calculation a machining supplier is better placed to run than a plating shop.
The stack-up, stated once
A coating specified as 8 µm minimum lands on both walls of a bore and on both flanks of a thread. On a diameter that’s a 16 µm increase before any tolerance on the deposit itself is considered. Machining to the middle of a 25 µm fit tolerance and then plating to SC3 doesn’t leave a tight fit, it leaves an interference.
Thickness Build-Up and Two-Sided Stack
Diametral effect of the four ASTM B633 service-condition classes. Values are the arithmetic doubling of the class minimum; the deposit tolerance band your plater works to sits on top of these.
| Class | Min. deposit, one surface | Diametral increase | Effect on an ISO h7 fit at 20 mm |
|---|---|---|---|
| Fe/Zn5 (SC1) | 5 µm | 10 µm | Consumes roughly half of a 21 µm h7 band |
| Fe/Zn8 (SC2) | 8 µm | 16 µm | Consumes most of the band; pre-plate dimension must move |
| Fe/Zn12 (SC3) | 12 µm | 24 µm | Exceeds the band; the fit must be re-cut before plating |
| Fe/Zn25 (SC4) | 25 µm | 50 µm | A different fit class or a masked surface is required |
Significant Surfaces, Threads and Blind Holes
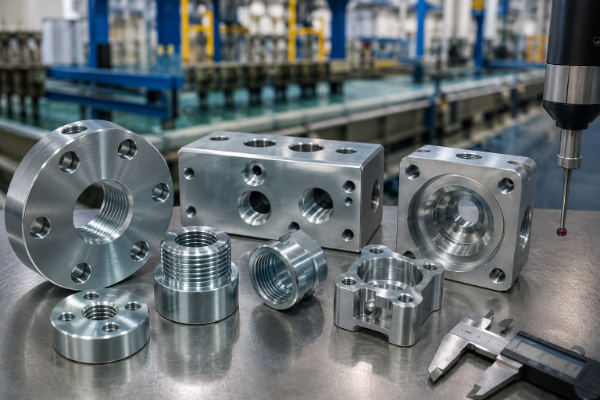
ASTM B633 clause 7.1.2 carries a rule that surprises most buyers: threads, holes, deep recesses and the bases of angles are normally exempt from the minimum thickness requirement unless the drawing designates them. If your customer’s inspector measures in a thread root and rejects, the drawing, not the plater, created the dispute.
- Note 4 of the same standard warns that the dimensional tolerance of most threaded articles doesn’t permit much more than 8.0 µm of coating, and heavier coatings require the build-up to be allowed for during manufacture
- ASME B1.1 Class 2A applies its size limits for a standard external thread before coating, and the allowance may absorb the coating only if the maximum coating thickness is no more than one quarter of that allowance
- API 20E rules that for petroleum and natural gas bolting, “oversizing of nut threads or under-sizing of bolt threads is not permissible”
- Blind holes and deep recesses must be nominated as exempt or as significant on the drawing, because silence defaults to the clause 7.1.2 exemption and that default is rarely what the designer meant
A conflict that lives inside your own specification stack
Read those three rules together and they don’t agree. The whitepaper authors who assembled them say so directly: “While the ASME standard is accepted, it directly contradicts the API specification and the BSEE guidelines.” A supplier who notices the contradiction at drawing review saves a rejection; a supplier who plates to the drawing and ships doesn’t.
ISO 4042:2022 is the counterpart for fasteners, and its 2022 revision states that its requirements take precedence over other documents dealing with electroplating. That revision also deleted every reference to ISO 2081:2018 and ISO 19598:2016 for the express purpose of removing contradictions between them. When a European customer names ISO 4042 and a US customer names ASTM B633 on the same assembly, that precedence clause is the tie-breaker.
Hydrogen Embrittlement Relief for High-Strength Steel
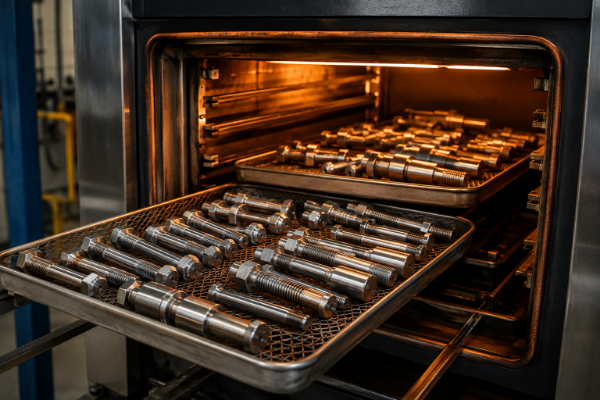
Hydrogen embrittlement can appear after delivery, so material strength, cleaning and plating route, relief requirements, timing and acceptance evidence must be resolved before release.
Information Required for Embrittlement-Relief Review
State the substrate, tensile strength or hardness, plating process, cleaning route, relief temperature, duration and maximum delay after plating.
The written quotation must identify each responsible processor and the records required to demonstrate the agreed route.
What triggers the requirement and what governs it. What governs is the standard, not the shop-floor habit — and the two are not the same document.
| Trigger | Requirement | Source of the rule |
|---|---|---|
| Machined, ground, cold-formed or cold-straightened part at or above 1000 MPa (31 HRC) | Stress relief before plating | ASTM B633 clause 6.4 |
| Steel above 1700 MPa (247 ksi, 46 HRC) | Shall not be electroplated | ASTM B633 clause 1.3 |
| Hardened steel after plating | Embrittlement relief bake before any supplementary treatment, started within 4 hours of removal from the last process | ASTM B633 clause 6.5 |
| The bake schedule itself | Temperature and duration set by tensile strength — B633 defers the schedule rather than fixing a number | ASTM B850 Table 1, referenced by B633 |
| Common commercial practice on shop pages | 375°F ± 25°F for a minimum of 8 hours above about 36 HRC | Plater practice, not the governing standard — and 8 hours is not 3 |
That last row is the point. That three-hour bake in the engineer’s specification sits below what working platers commonly run, and the standard defers to a strength-based schedule rather than blessing either number. This is exactly the kind of gap a drawing review catches and a purchase order doesn’t.
What Electroplating Cannot Do: Trade-Offs Worth Knowing Before You Specify
No competitor page in the top five of this category states a single limitation of the process they sell. That silence is a differentiator we’re happy to take, because a buyer who discovers a limit after the purchase order treats it as a defect rather than a property.
Six limits of electroplating as a process, each with the second-order cost it creates.
Property
Zinc
Zinc-nickel
Electroless nickel
Hard chrome
Protection mechanism
Sacrificial
Sacrificial, alloyed
Barrier
Barrier
Governing specification
ASTM B633 / ISO 2081
ASTM B841
Autocatalytic nickel-phosphorus specification named by the customer
Engineering chromium specification named by the customer
Thickness the spec sets
5 / 8 / 12 / 25 µm by service condition
Set by ASTM B841 class; confirm against the named specification
Confirm against the named specification
Confirm against the named specification
Minimum salt spray in the spec
12–120 h by finish type
Suppliers cite roughly 5–6× zinc at equal thickness; not a contract term
Not expressed as a salt-spray threshold in the deposit spec
Not expressed as a salt-spray threshold in the deposit spec
Deposit hardness
Soft, ductile
350–450 kg/mm² Vickers
Rises sharply after heat treatment; confirm against the named specification
The hardest of the four; confirm against the named specification
Coverage in deep recesses
Throwing power depends on bath; alkaline better than acid
Alkaline chemistry covers recesses well
Uniform without regard to current path — the reason it wins on complex geometry
Poor; current concentrates on edges
Thread and fit behaviour
Build-up consumes the allowance directly
Same build-up problem, plus higher torque for a given preload
Uniform build-up is easier to predict on a thread
Usually ground after plating rather than plated to size
Hydrogen embrittlement exposure
High on hardened steel; bake required
High; porous deposit is designed to vent hydrogen during bake
Lower — the process is autocatalytic rather than current-driven
High on hardened steel; bake required
Where it wins on a machined part
Volume steel parts in general industrial duty
Alloy-steel parts in marine, automotive and defense duty
Valve bodies and internal bores where uniformity matters more than hardness
Wear surfaces, hydraulic rods, shafts
The counter-intuitive one
Conventional direct-current zinc-nickel is made deliberately porous so hydrogen can escape during the relief bake. That same porosity raises the chance of hydrogen re-entering the substrate during in-service corrosion unless a polymer topcoat is added, and the rougher surface needs higher torque to reach a given preload. A fix for one failure mode created the conditions for another, which isn’t always how a supplier will describe it.
On the very large salt-spray numbers you may have seen
Published work on a pulse-plated nanostructured zinc-nickel process reports no red rust to roughly 7,200 hours on panels and 8,000 hours on bolts. Those results are a specific proprietary process tested under a modified ASTM B117 method, they do not generalise to zinc-nickel as a family, and they are not a finish Zhenling Metal delivers. We repeat the qualifiers because dropping them is how a research figure turns into a false capability claim.
SPECIFICATIONS
Records to Specify and Confirm for the Order
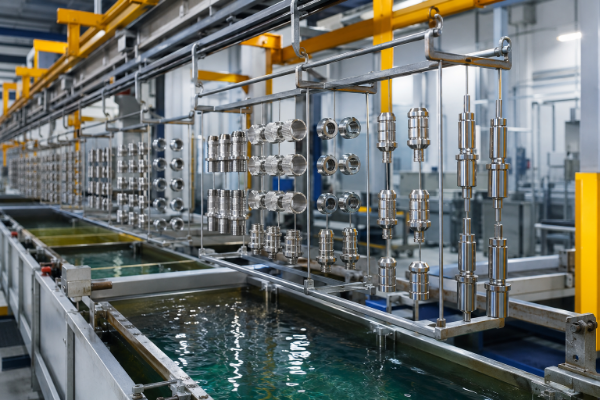
For an overseas order, specification transfer, processor responsibility, measurement location, record scope, packaging and communication points must be confirmed in the written quotation before release.
Records to include when specified in the written quotation [Hover to reveal list]
- Approved drawing revision and plating callout, including significant surfaces, when this controlled copy is specified for delivery
- Material document from the named issuer, with agreed heat or lot linkage, when specified for the order
- Applied finishing specification, edition, service condition and finish type when the quotation includes a process record
- Coating-thickness results, measurement method and locations when inspection reporting is specified
- Embrittlement-relief record and timing relative to plating when required and included in the written quotation
- Pre-plate or post-plate dimensional report for agreed critical features when included in the order
Where the Reading Is Taken Decides Whether the Lot Passes
Location is settled before number, because ASTM B633 measures the minimum on significant surfaces and exempts thread roots, blind holes and deep recesses unless the drawing designates them. A reading on the flange face of a valve body and a reading 0.5 mm inside its bore can differ by more than the entire 12 µm class. Unlike a general appearance check, that is a dispute nobody can settle once the parts have shipped.
Built around the drawing, not around the invoice
When the written quotation includes a record package, it must identify the controlling drawing revision, agreed measurement points, material-document issuer and linkage, finishing specification and edition, processor responsibility and report scope. No record is implied unless it is listed for the order.
The mistake we see most often is a purchase order that names a coating class and never names where it’s measured. Where the drawing is silent, the standard’s exemption applies by default, and that default is rarely what the designer intended. Reading the callout back before release costs a query cycle; a rejected lot costs the parts.
Verification methods and what each one can and cannot settle.
| Method | Reads | Limit |
|---|---|---|
| X-ray fluorescence | Local thickness, non-destructive, fast | Needs a flat enough spot and a calibration for the alloy; struggles inside recesses |
| Magnetic induction | Non-magnetic coating on a steel substrate | Substrate permeability and surface curvature both shift the reading |
| Microscopic cross-section | The true local thickness, including in a thread root | Destructive; one part is consumed per reading |
| Neutral salt spray to the named type | Whether the finish clears the acceptance threshold in the standard | Says nothing about service life; the hours are a contract term |
If a lot does not conform
The route is fixed in advance rather than negotiated after: quarantine the lot, identify whether the cause sits at machining, pre-treatment or deposition, and hold the disposition decision with you rather than at the finishing subcontractor. Zinc plating is one of the few finishes that can be stripped and re-run without scrapping the part, which is why the deposit family and the recovery path are decided together.
Want the record set defined before the first purchase order?
Send a Drawing for a Finish-Spec Review →Certifications, Compliance and Scope Boundaries
Supplier qualification and electroplating process requirements are separate checks. Any credential must be verified by legal owner, site, number, scope and validity, while the applicable finishing specification, edition and acceptance criteria are controlled by the drawing, purchase order and written quotation.
CE-RELATED REQUIREMENT
Verify owner, site, number, scope, validity and order applicability
ASME-RELATED REQUIREMENT
Verify owner, site, number, scope, validity and order applicability
Since 2006
Shanghai Zhenling Hardware Co., Ltd., factory in Jiashan, Zhejiang
8,000 m²
Plant area with 6,000 m² of workshop
5-axis CNC
Imported 5-axis machining centres alongside 3- and 4-axis machines
ORDER-SPECIFIC
No production-volume or export-share claim; confirm capacity and destination scope per order
- Machining of the component, from blueprint or sample, in the material grades listed on this page
- Review of the plating callout against the standard your customer named, before release
- The written quotation identifies finishing coordination, processor responsibility, delivery scope and commercial line items
- Pre-plate dimensional planning so the finished part lands inside the drawing, not beside it
- Stress relief and embrittlement relief routing where the strength and hardness of the part trigger it
- The quotation must identify whether each finishing step is performed in-house or by a named outside processor and who owns qualification and records
- This page does not claim a CE- or ASME-related credential for Zhenling; any credential required for qualification must be verified for the named entity, site and order
- No plating capacity, minimum order quantity, yield or lead time is fixed on this page; confirm each commercial assumption in the written quotation
- Decorative work such as gold plating services and jewellery finishing sits outside this scope entirely
- We won’t quote a salt-spray hour count as a property of a part we haven’t tested
Compliance obligations travel with the chemistry rather than with the supplier. RoHS and the end-of-life vehicle directive restrict hexavalent chromium, which OSHA describes as capable of causing severe health effects including lung cancer in electroplating work, and that is why trivalent passivates now carry most new automotive and electronics work, and why a drawing that still names a hexavalent finish should be challenged before it is quoted.
Environmental impact, and what it changes for a buyer
The environmental impact of metal electroplating is a cost centre rather than a talking point: the manufacturing process consumes electricity, generates permitted wastewater, and is costly to run in line with current manufacturing practices. In the United States the process itself sits under a National Emission Standard for Hazardous Air Pollutants, 40 CFR Part 63 Subpart N, which limits chromium emissions from hard chromium, decorative chromium and chromium anodizing tanks to the maximum achievable control technology level. Less harmful chemistries have replaced several older ones for exactly that reason. A buyer gains by naming an environmentally current chemistry at design stage rather than being told late in a programme that a bath is no longer offered.
Why the boundary is published rather than blurred
Do not infer electroplating capability or compliance from an unrelated supplier credential. Verify the legal owner, site, number, scope and validity of any required qualification, then control the machining, finish callout, outside-process responsibility and delivered evidence through the written quotation.
Need the scope boundary in writing for your supplier file?
Send a Drawing for a Finish-Spec Review →
and we’ll state it against your part.
Procurement Guide: Cost Drivers, Lead-Time Variables and RFQ Requirements
Not one of the three highest-ranking pages in this category explains how a finishing quote is built. That opacity is what makes electroplating services cost feel arbitrary to a buyer, and it’s the easiest thing on this page to fix. Below are the variables that move the number, without a number attached to any of them.
Cost drivers in a plated machined part.
Each row is a variable you control at drawing stage.
Driver
How it moves the quote
Service condition class
SC4 at 25 µm puts five times the metal on the part that SC1 at 5 µm does, and takes proportionally longer in the tank
Finish type and passivate
A Type VI colored passivate at 120 h is a different chemistry and a different line pass than a Type III at 12 h
Rack or barrel
Racking is handling time per part; barrel work is priced per load
Surface area, not part count
Deposition is charged against area; a hundred small plugs may cost less than one flange
Masking
Every surface that must stay bare is manual work repeated on every piece
Embrittlement relief bake
Adds an oven cycle measured in hours and a record that has to be produced
Inspection method named
An X-ray reading is minutes; a cross-section consumes a part and a technician
Lot size and release pattern
Split releases repeat setup; a single lot amortises it once
The trade-off buyers get wrong on this table
Dropping from SC3 to SC2 saves metal and tank time, but the eight-year sacrificial reserve you calculated from the corrosion rate drops with it. The cheapest line on a finishing quote isn’t always the cheapest part over its service life, and the arithmetic that settles it’s in the Service-Condition Ladder above rather than in the quote.
Where electroplating is used, and which of those uses we serve
Electroplating is used across industries wherever a base metal is asked to do a job its own surface can’t. Uses of electroplating in various industries run from structural fasteners to electronic components, and no supplier serves that whole variety of industries equally well. Ours is the industrial subset, so the table states which parts of it we machine and finish rather than claiming all of it.
Industry
Typical parts
What governs acceptance
Oil and gas industry
Flanges, valve bodies, plugs and bent pipe in separation and fluid-control duty
API bolting rules, thread allowance, safety and performance qualification
Automotive industry
Chassis, brake and general machinery components — high-volume steel products in fitted assemblies
Trivalent passivates, end-of-life vehicle restrictions
Aerospace industry
Alloy-steel high-performance precision parts and landing gear hardware
Low-hydrogen-embrittlement chemistry, ASTM F519 style acceptance
Medical equipment industry
Stainless and nickel alloy instrument bodies and instrumentation housings
Often no coating at all — passivation instead
General manufacturing
Plating for fasteners, machined assemblies, and any metal part with a fitted feature
ISO 4042 precedence, ASME B1.1 allowance
One deposit serves different industries for various applications, which is why a finish that’s routine in one is unusual in another. Automotive and aerospace demand drives most of the zinc-nickel work we see, whereas automotive applications alone drive most trivalent passivate demand, and aerospace applications add the embrittlement record burden on top. That difference in specification stack, rather than the deposit itself, is what moves the quote.
What lengthens the schedule
Lead time moves with the same variables plus three more: an incomplete callout that forces a query cycle, a bake requirement that adds an oven pass, and a re-work loop caused by a fit that was never planned for the deposit. We publish no day count here because we hold no first-party lead-time data for this scope, and inventing one would be worth less to you than knowing which factors move it.
What a quotable RFQ contains
1
Drawing with the plating callout: standard number and date of issue, service condition, finish type
2
Any significant surfaces marked, and any thread or blind hole designated as included or exempt
3
Substrate grade, and tensile strength or hardness if above 1000 MPa
4
Fit class on any plated diameter, so the pre-plate dimension can be planned
5
Inspection method and acceptance criteria, including who witnesses what
6
Annual volume and release pattern
7
End market, because RoHS, end-of-life vehicle and API rules change the answer
Machining and finishing are quoted together because splitting them is what creates the gap both suppliers then point at. If the pre-plate dimension is our decision and the deposit is someone else’s, the fit is nobody’s. See how the pre-plate dimension is held on the machine before it ever reaches a tank, or browse the full range of finishing routes we coordinate for parts that need something other than plating.
Searching for an industrial electroplating company when the part still has to be machined first?
Request a Machining + Finish Quote →
and both halves are quoted against one drawing.
Electroplating Engineering Tools
Technical engineering utilities for evaluating plating specifications, tolerances, and post-process heat treatments.
Quote the machining and the finish together
Send the drawing and the annual volume. You get the plating callout read back against the standard your customer named, the pre-plate dimensions planned around the deposit, and one supplier holding both ends of the tolerance chain.
Electroplating Services: Buyer Questions
These ten questions are the ones that arrive from real buyers and from the search results around this category, rather than the ones that make the service look good.
It’s quoted against surface area, service condition class, finish type, masking and lot size rather than per part, which is why a single flange can cost more than a hundred small plugs. We won’t print a price band on a public page for work that’s quoted per drawing. Send the drawing and the annual volume and you get a number instead of a range.
Look for ASTM B841 rather than B633 in the callout, or for a cadmium replacement clause, or for a marine, defense or under-bonnet application note. If the drawing names only “zinc plate” with no standard, nobody knows yet, and that is the query cycle worth having before the purchase order rather than after.
More, in every published account, driven by nickel content and tighter bath control. We hold no traceable first-party multiple and won’t invent one.
No. On a mild indoor part it buys corrosion performance you will never use while adding cost, torque variability and a porous deposit whose second-order behaviour has to be managed. Zinc-nickel earns its place where the service condition earns it, and ASTM B841 exists as a specification separate from B633 precisely because a 12–18% nickel alkaline deposit is a cadmium replacement for high-duty steel rather than a general-purpose upgrade. Hardness in the 350–450 kg/mm² Vickers band is worth paying for on a brake caliper and worth nothing on an indoor bracket. The honest test is the service environment in ASTM B633 Appendix X1, not a preference for the more advanced-sounding finish.
Yes, and it adds one of its own. Zinc-nickel still consumes the thread allowance under the ASME B1.1 quarter-of-the-allowance rule, and the rougher, harder surface commonly needs higher torque to reach the same preload. Plan the pitch diameter before plating and specify the lubricant condition at assembly.
They can, but dissimilar sacrificial coatings sharing a wet joint form a galvanic couple and the less noble deposit goes first. Isolate the interface.
Zinc-nickel is not the question here, the passivate on top of it is. Specify a trivalent passivate rather than a hexavalent chromate and the finish clears RoHS and end-of-life vehicle restrictions. A drawing that still names a hexavalent chromate for an EU-bound part should be challenged before it is quoted.
ISO 2081 is the counterpart for electroplated zinc coatings on iron and steel. For fasteners specifically, ISO 4042:2022 takes precedence over other documents dealing with electroplating, and its 2022 revision deliberately removed references to ISO 2081:2018 to stop the two standards contradicting each other on embrittlement and baking. On a mixed EU and US assembly, name one and state which governs.
Type and thickness are two separate fields in this standard, and mixing them is the most common callout error we see. Type III is a colorless chromate finish carrying a 12-hour minimum salt spray, and it says nothing at all about how thick the zinc underneath it is. Thickness comes from the service condition class instead: SC1 mild is Fe/Zn5 at 5 µm, SC2 moderate is Fe/Zn8 at 8 µm, SC3 severe is Fe/Zn12 at 12 µm, SC4 very severe is Fe/Zn25 at 25 µm. Watch one detail here. Several vendor pages and generative answer panels print the SC3 minimum as 13 µm, while Table 1 of ASTM B633-13 states 12. A complete callout names the standard, the date of issue, the service condition and the type.
Both are clear finishes, and they aren’t interchangeable. Type III is a colorless chromate with a 12-hour minimum salt spray; Type V is a colorless passivate at 72 hours, and the passivate route is the hexavalent-free one. If a drawing says “clear zinc” without a type, the difference between those two numbers is a factor of six on the acceptance test.